Your shopping cart is empty!


"The Recognized Technical Experts in Our Field"
Raw Active Pharmaceutical Ingredients (APIs) are highly sensitive bulk chemical powders that are vulnerable to clumping, caking, hydrolysis, and microbial growth. IMPAK's experts know that proper packaging for these high-value products goes beyond simple moisture absorption to encompass critical compliance, equipment integration, and stability systems.
IMPAK not only produces robust specially-formulated desiccant media and high barrier materials that virtually eliminate permeation of moisture. We also have decades of experience to draw from when customers need partners who can solve their specific packaging challenges.
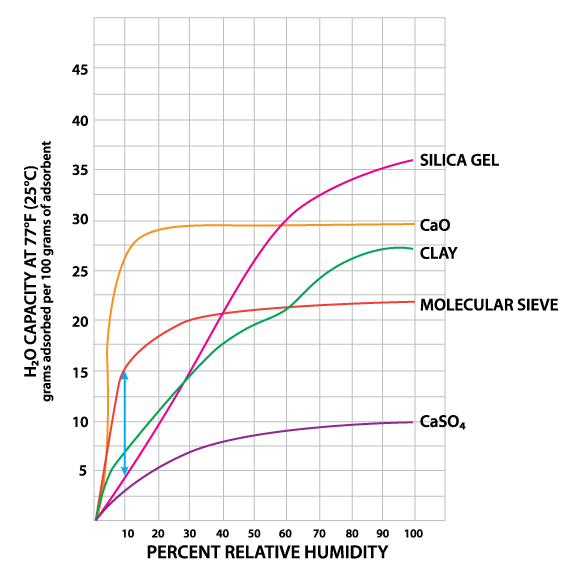
Ultra-Low Humidity Targeting: While standard silica gel operates efficiently down to 5% relative humidity (RH), IMPAK provides specialized molecular sieve desiccants capable of achieving near 0% RH, which is essential for moisture-sensitive bulk API storage.
Targeted Pore Size Customization: We engineer solutions across specific pore sizes (3A, 4A, 5A) to ensure selective moisture adsorption without extracting or reacting with volatile API components. Read more about molecular sieve
FDA & cGMP Strict Compliance: All sorbent and high-barrier packaging solutions meet non-toxic, non-corrosive FDA and EU REACH/RoHS standards for direct and indirect pharmaceutical contact.
Accelerated Stability Testing: IMPAK products guarantee protection designed to help your drugs pass rigorous ICH Q1A long-term and accelerated stability protocols, significantly streamlining time-to-market.

Space-Saving Active Formats: IMPAK supplies cutting-edge embedded formats including specialized containers and integrated desiccant packaging, offering active-barrier protection for a variety of challenging production scenarios.
Smart Traceability & Data Integration: IMPAK is continually developing intelligent packaging options, incorporating color indicators, QR codes, and anti-counterfeit print to deliver complete transparency across global pharmaceutical supply chains.
These 10" x 16" pouches, made from our 7.5 mil ultra high barrier PAKDRY7500 material, were manufactured for a pharmaceuticals producer who wanted a quick and easy means of distinguishing sealed ingredients on their production floor.
Whether you require ultra-low moisture protection, specialized barrier laminations, or integrated desiccant packaging, IMPAK Corporation delivers the technical expertise and quality assurance your pharmaceutical packaging requires.


